 StampPro
Built to Run.
Built to Last.
Built to Ten-
Thousandths.
Progressive and transfer dies for automotive tier-one, medical device, and contract manufacturers. Every station engineered to spec. Every hit documented.
4.2M+
Hits Before Sharpening
1.4 μm
Surface Finish Ra
38 yr
Shop Experience
Inspection Status
FIRST ARTICLE APPROVED — LOT 2026-047
Cpk
1.67
AMBA Member
Die Excellence Award
4.2 Million Hits
Before First
Sharpening.
That number isn't marketing — it's the median tool life across our D2/M2 progressive die builds in HSLA 590. Documented in SPC. Verified by customers running 24/7 lights-out cells.
Max Press Tonnage
Servo & mechanical press cells
Max Station Count
Progressive and transfer tooling
Held Tolerance
Wire EDM ground & inspected
First-Hit Approval Rate
Across 847 production tools
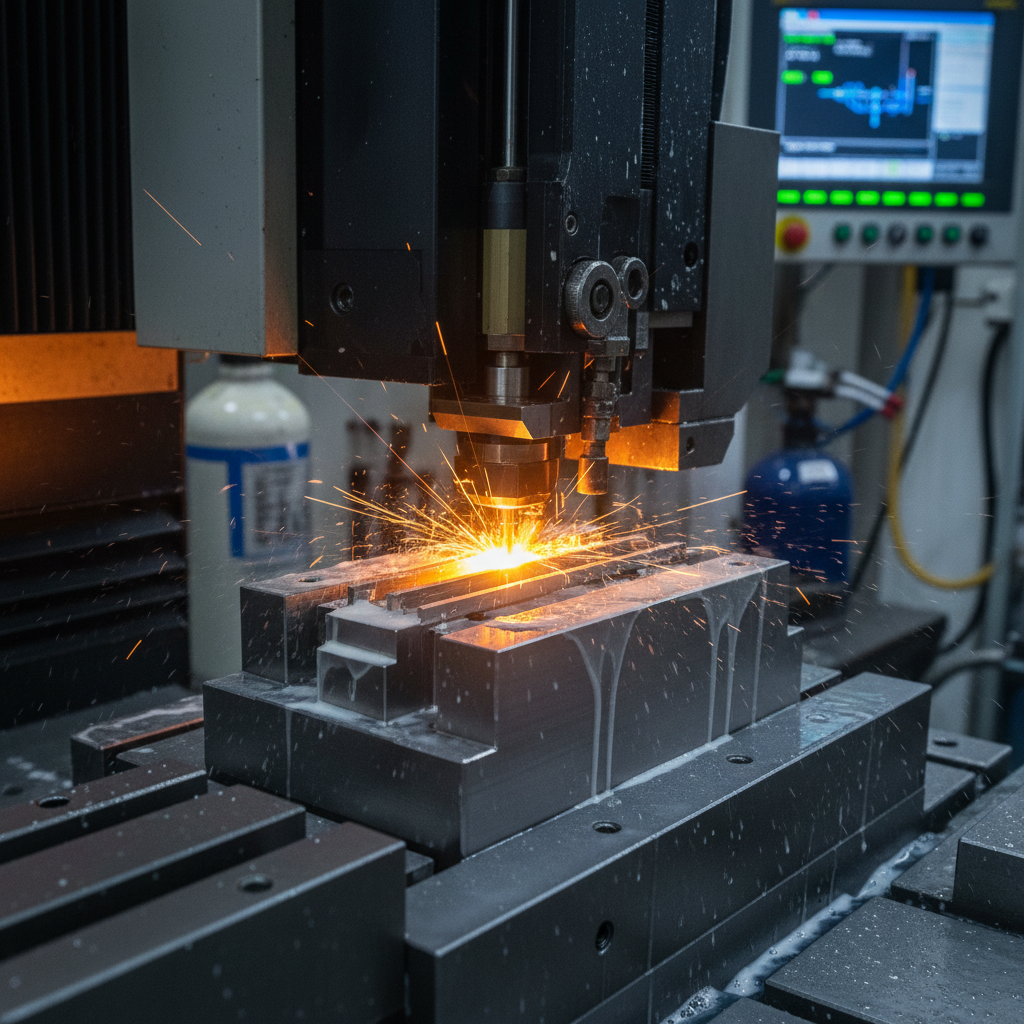
Wire EDM
±0.00005" Positional
Ra 0.2 μm surface
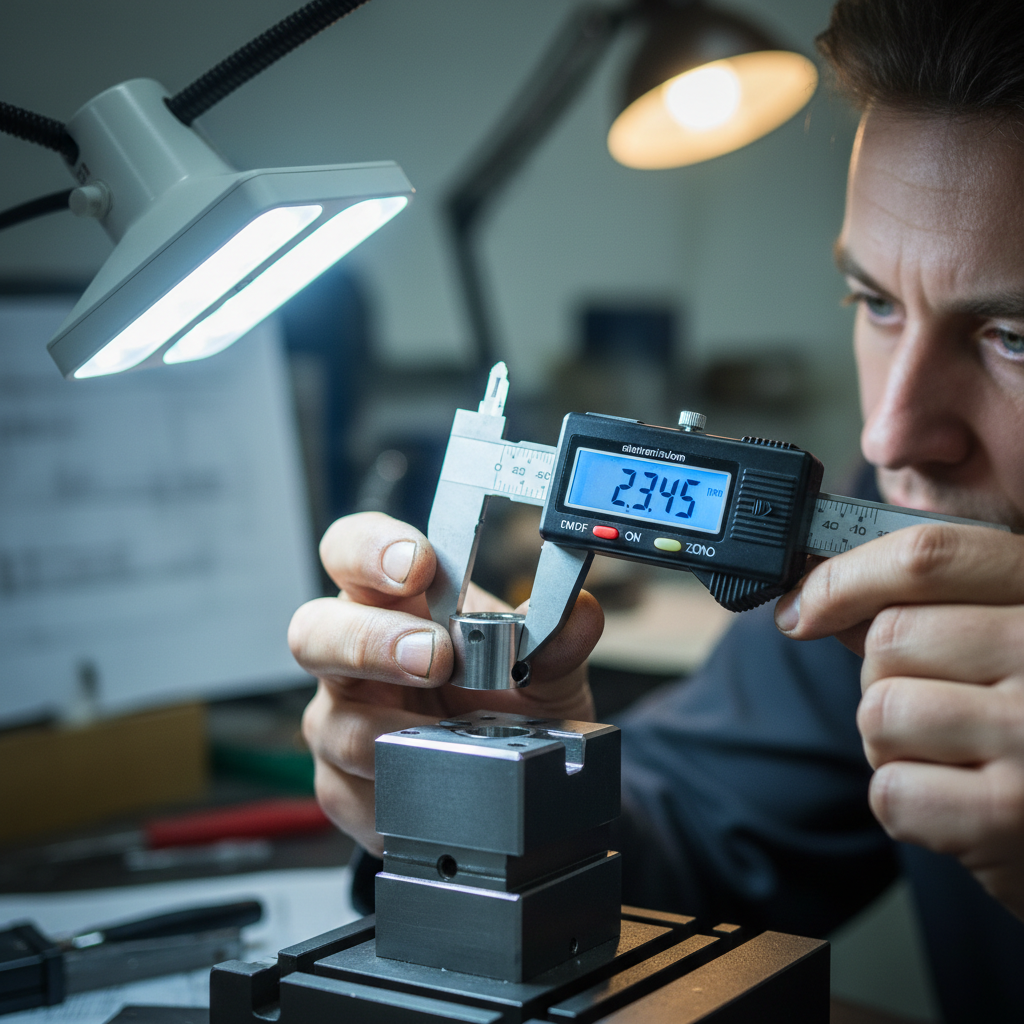
Zeiss Contura G2 · 100% FAI
If It Stamps,
We've Run It.
From 0.004" medical-grade titanium foil to 6mm HSLA structural blanks — our die steels and coatings are matched to your material before the first simulation pass.
Qualified Material Matrix
Every Station
Engineered.
Every Hit Logged.
Our process follows a white-paper cadence — DFM first, simulation before steel, CMM before assembly, SPC before shipment. The sequence is non-negotiable because rework at the press is 40× more expensive than rework on the screen.
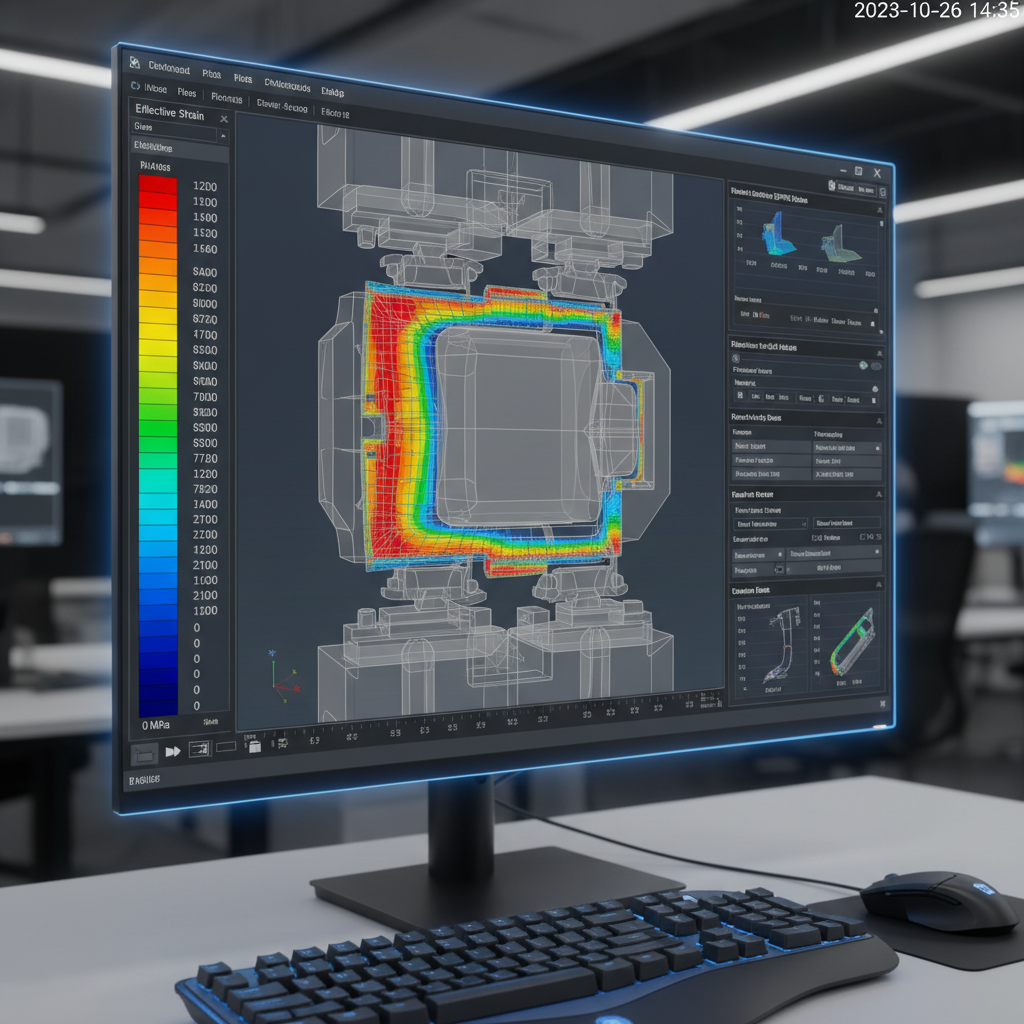
DFM Review & Simulation
We run your STEP file through AutoForm and Dynaform before touching steel. Formability, springback, thinning — every failure mode surfaced on screen, not on the press.
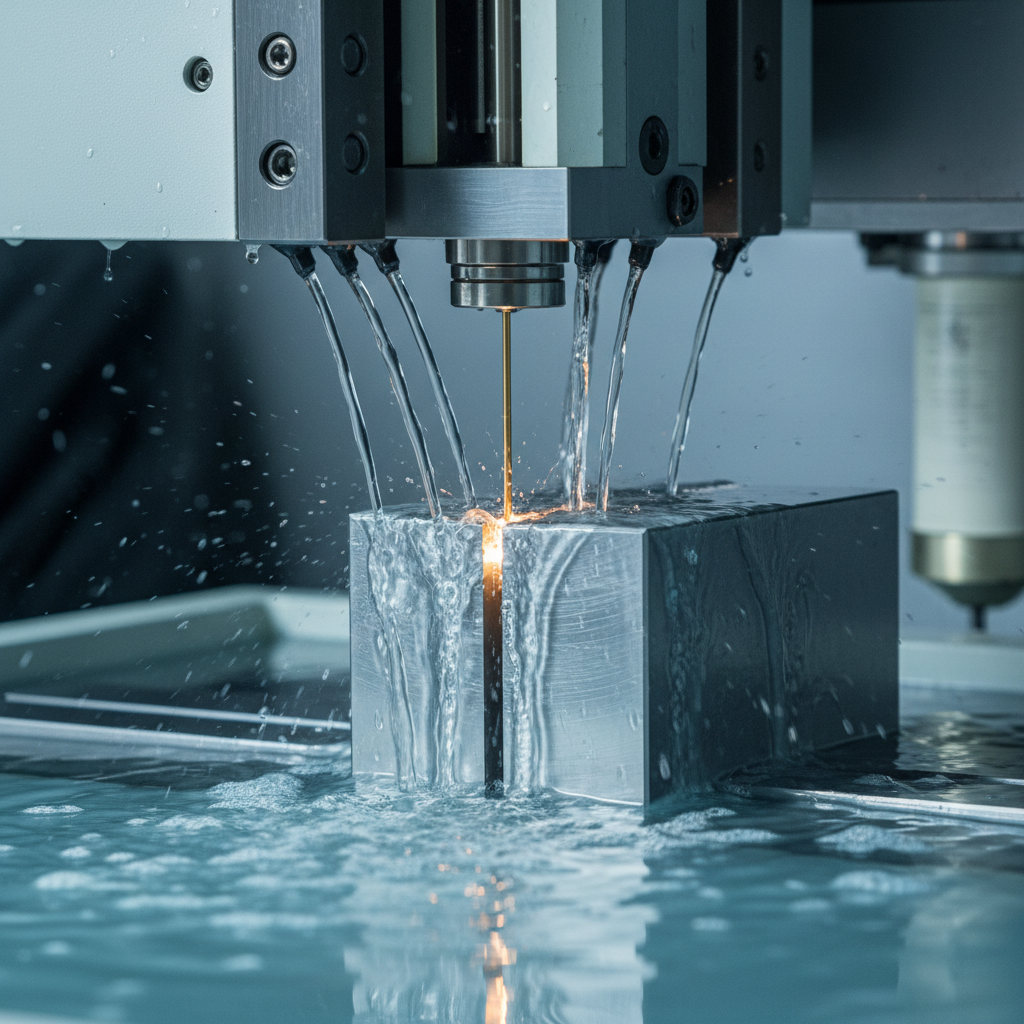
Wire EDM & Precision Grinding
Punch and die sections cut on Fanuc α-CiB wire EDM, then surface-ground on Studer cylindrical grinders. Every component CMM-verified before assembly.
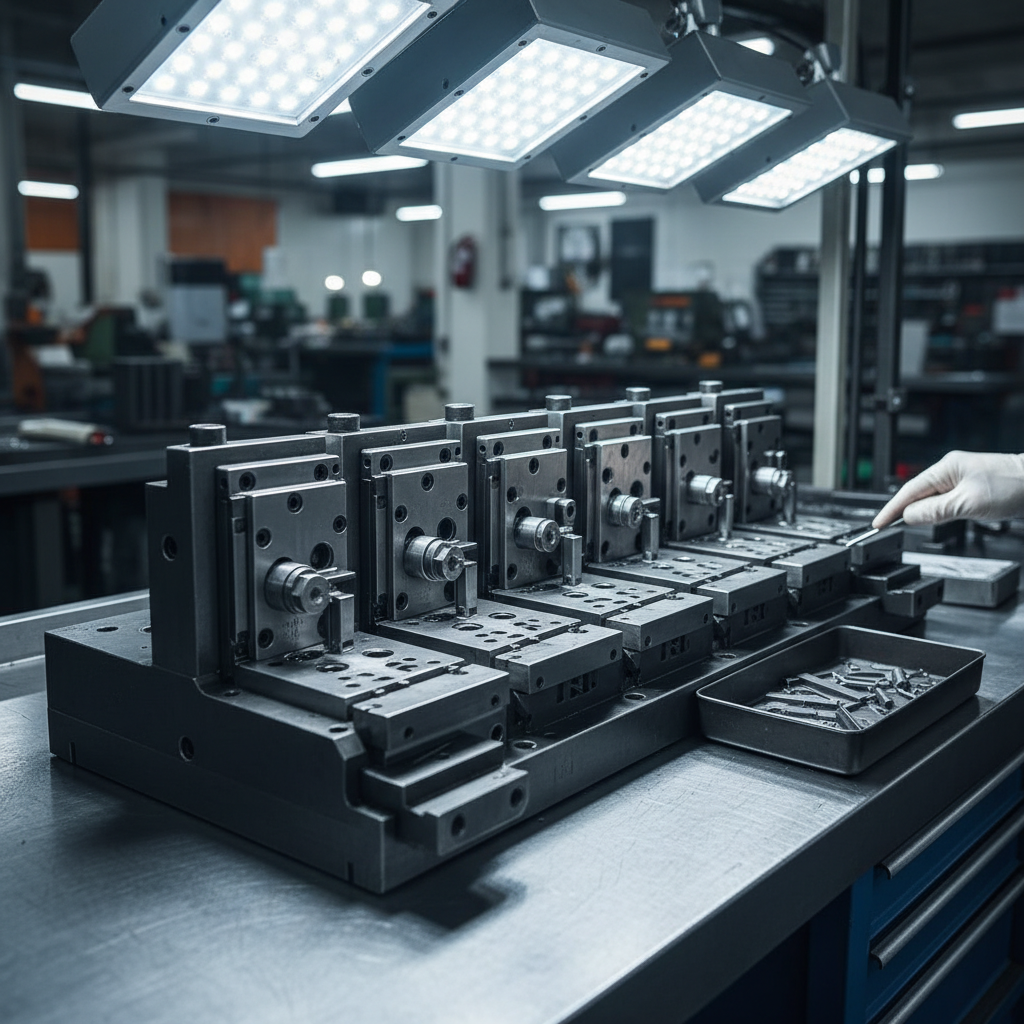
Progressive Die Build & Tryout
Assembly in a temperature-controlled build room. Tryout on our servo press cells with in-die sensors logging force signatures from hit one. We don't ship until Cpk ≥ 1.33.
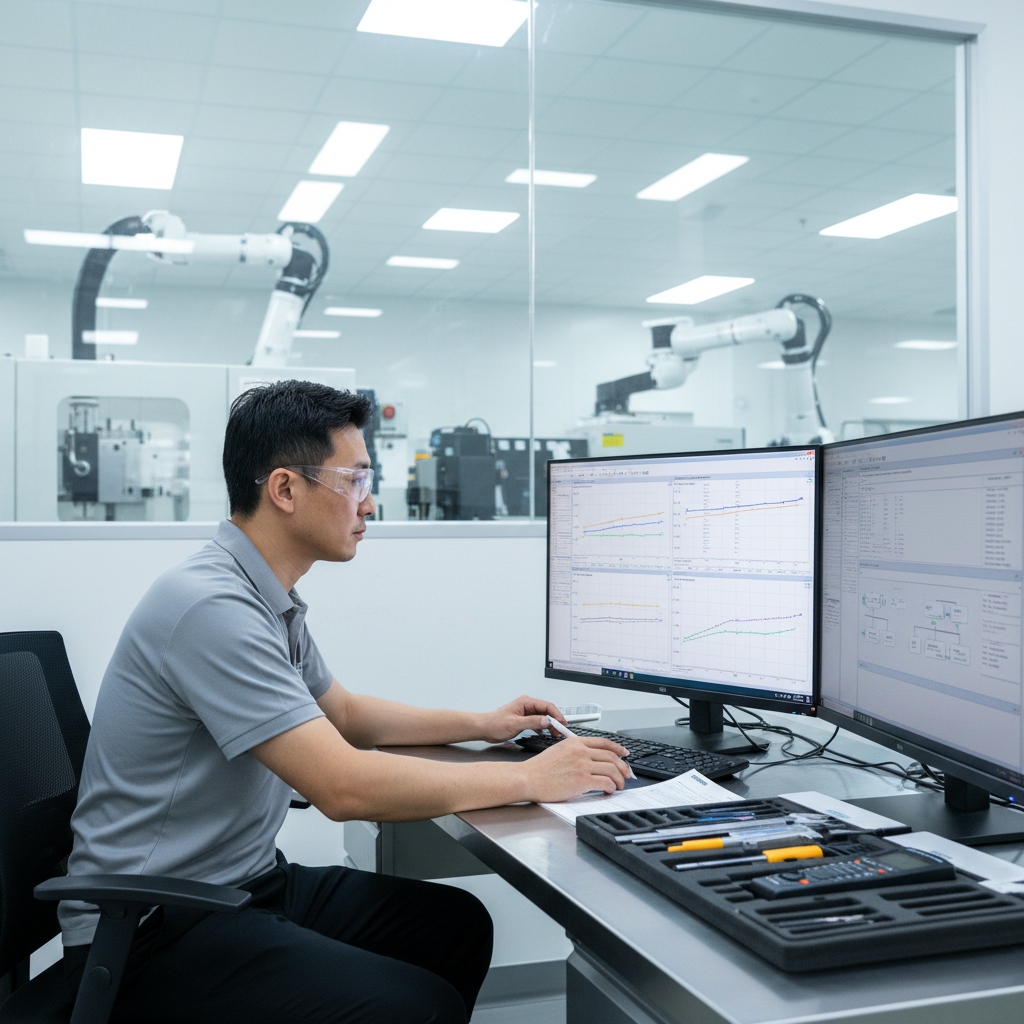
SPC Handoff & Production Support
Every tool ships with a complete SPC package — Xbar-R charts, Gage R&R, first article inspection report. Our field engineers are on-call for the first 500k hits.
Stop Evaluating.
Start Specifying.
Below are three production tools pulled from our SPC archive — real part numbers, real customer industries, real CPK values. Names anonymized at customer request; data is not.
Fleet-Wide Average
CPK Trend — 2021 to Present
Current Average
1.81
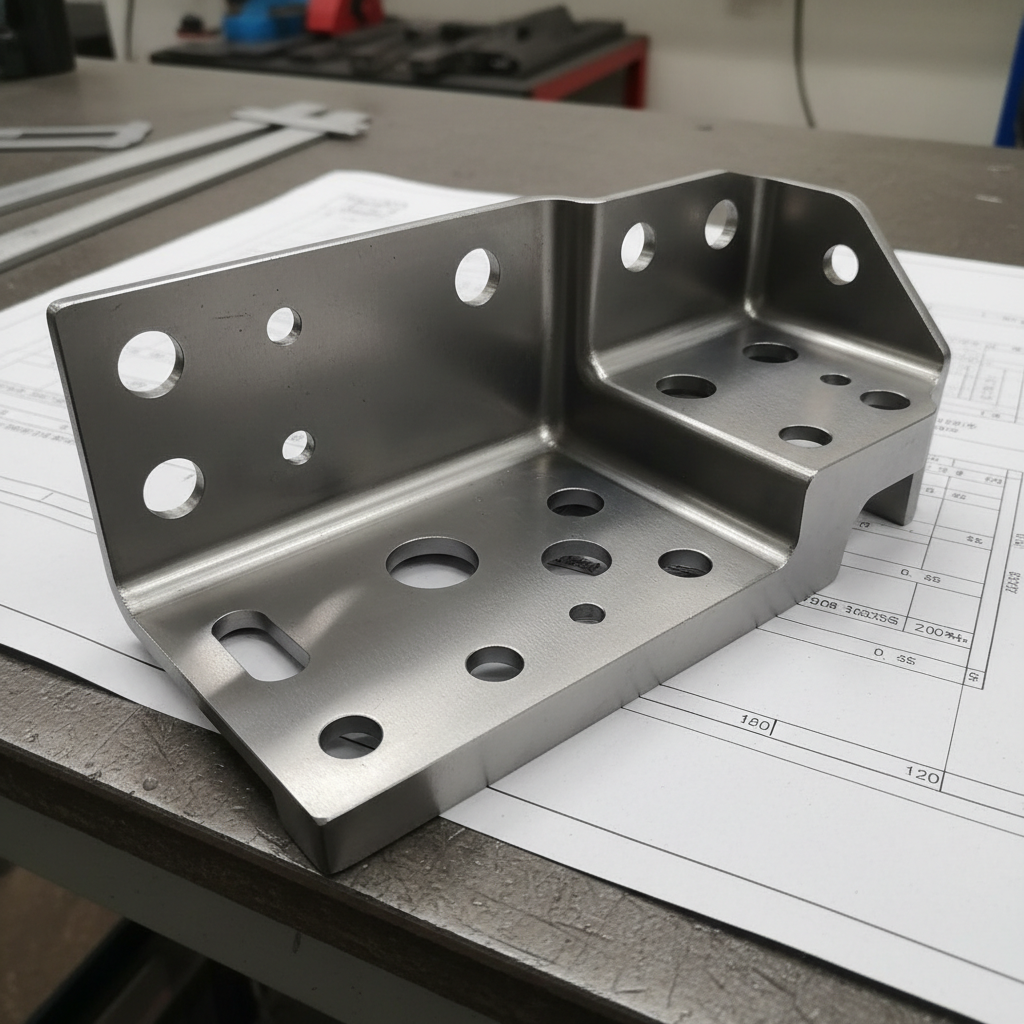
Part Number
P/N 8A-3472-B
Cpk
1.71
Tier-1 Automotive — Seat Rail Bracket
P/N 8A-3472-B
Material / Gauge
HSLA 590 MPa · 2.3mm
Annual Volume
1.2M parts/yr
Process Cpk
1.71
Tool Life
5.8M hits
Eliminated 3 secondary ops. Reduced scrap from 1.8% to 0.12%. Line speed increased from 48 to 72 spm after die optimization.
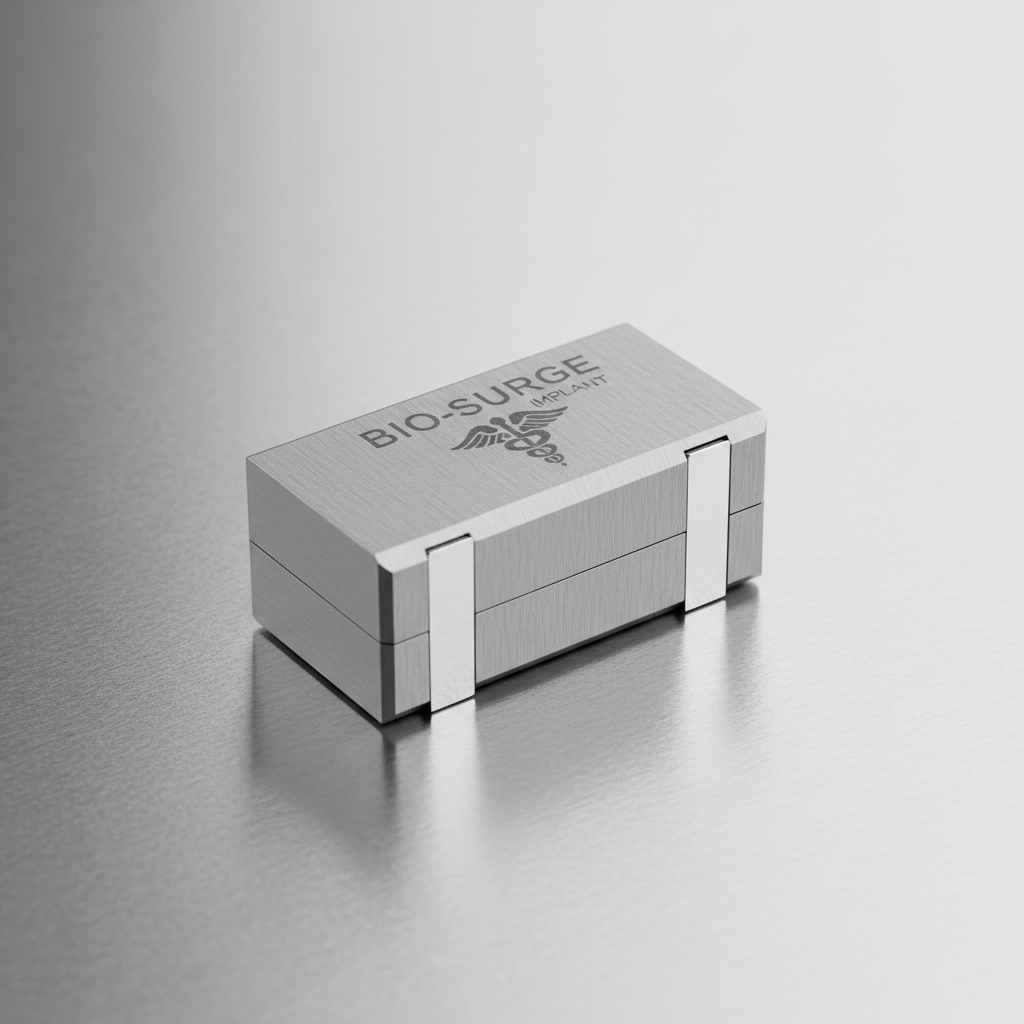
Part Number
P/N MT-0091-Ti
Cpk
1.89
Medical Device OEM — Surgical Clip Housing
P/N MT-0091-Ti
Material / Gauge
CP-Ti Grade 2 · 0.38mm
Annual Volume
4.5M parts/yr
Process Cpk
1.89
Tool Life
2.1M hits
Held ±0.0002" on critical clip geometry across 6 consecutive production runs. Zero field rejections in 18 months of distribution.
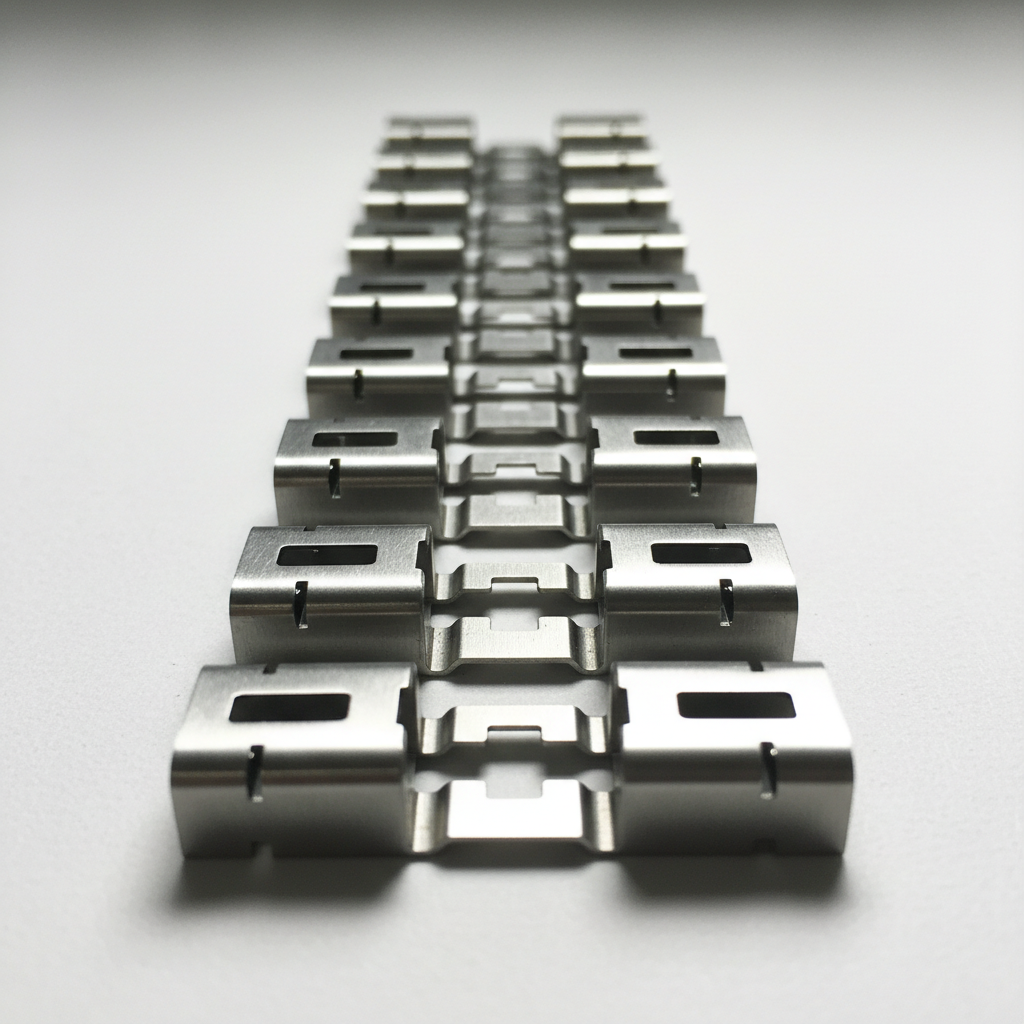
Part Number
P/N CE-7731-SS
Cpk
1.63
Contract Manufacturer — Connector Terminal
P/N CE-7731-SS
Material / Gauge
AISI 304 · 0.6mm
Annual Volume
18M parts/yr
Process Cpk
1.63
Tool Life
4.2M hits
Redesigned existing transfer die to progressive format. Cycle time reduced by 34%. CPK improved from 0.98 to 1.63 in first production run.
Send Us
Your Part
Print.
Material and thickness first. We'll have a preliminary DFM assessment back to you within 72 hours — no sales call required.
Still Researching?
Download Our Tolerance Guide
32-page PDF covering achievable tolerances by material, gauge, and die type. Includes CPK benchmarks and process selection matrix.
Ready to spec your next progressive die?
72-hour DFM turnaround · NDA before file review · CPK targets in quote